page-header

SPECIFICATION GUIDANCE

INTRODUCTION

Updating structural specifications to reduce embodied carbon can help a firm commit to lowering their carbon footprint on all projects. The way specifications are written can also drive market change, affecting the way manufacturers develop new materials. The greatest opportunities for large-scale embodied carbon savings require this to be considered in design decisions made at the earliest stage of a project. Design teams should strive to reduce material consumption as much as possible and then specify Lower Embodied Carbon, or Buy Clean, materials, but not rely on specifications alone.

While re-writing specifications can seem daunting, there are a variety of ways specifications can be revised to potentially reduce embodied carbon ranging from simple changes to complete overhauls. Different strategies may work better for different firms and different types of projects. Compiled below is a list of tips and strategies that have been successfully used by structural engineering firms and material experts to reduce embodied carbon with specifications.

Disclaimer: The goal of these procurement guidelines is to help committed firms reduce the structural embodied carbon of their projects. The authors of these guidelines strive to balance information from multiple sources to provide impartial recommendations based on the current state of the industry. SE 2050 does not endorse any specific strategy or recommendation; best practices are for individual firms to decide.

Tips from the experts…

  1. Embodied carbon reduction requirements can be incorporated within standard material specifications, or as an addendum to be included on a select project basis.
  2. Early communication with both the client and the entire project delivery team is critical to meeting embodied carbon reduction goals.  Consider including a meeting during the design process on project embodied carbon goals as a specification requirement.
  3. Host an embodied carbon charrette and/or provide a cover letter to the General Contractor and/or preconstruction manager that includes an introduction to embodied carbon and the embodied carbon goals for the project.  This is especially important in regions where manufacturers and suppliers are unfamiliar with embodied carbon. (Note: the cover letter would be for information only and not considered a contract document.)
  4. Re-evaluate concrete specifications to eliminate unnecessary prescriptive requirements on materials such as minimum or maximum cement content, minimum or maximum fly ash or slag content, maximum w/cm ratio, etc. Consider specifying only performance requirements, such as compressive strength and exposure class.
  5. Specifications ultimately need to allow for competitive bidding. This is important to keep in mind as specification updates are made.
WHOLE BUILDING STRATEGIES

Promote Transparency and Disclosure
Requiring contractors to provide product-specific EPDs (Environmental Product Declarations), or similar product information disclosures, allows for the designer to understand and compare environmental impacts between suppliers.  This EPD product data must be included in a subcontractor’s bid.  The data can then be used to pick the subcontractor with the lowest Global Warming Potential (GWP) product. See Performance Specifications for guidance on setting GWP maximums in specifications.
Requiring EPDs will also help drive market change, and normalize the adoption of EPDs as a resource to make more informed design decisions.  The EC3 tool can help project teams gain easy access to a wide-variety of producer EPDs in one convenient location.
As an alternative approach to requiring product-specific EPDs from contractors, specifications can ask the contractor to provide industry-wide EPDs, or specifications can request, in lieu of requiring, product-specific EPDs.  If performing an LCA, the practitioner should be sure to update data sources to reflect the procured products and/or if material substitutions occur.

Transportation
Firms may consider specifying a maximum transportation distance to reduce the carbon footprint of shipping materials to the project site.  Materials are not always readily available regionally and may need to be shipped long distances, ultimately adding more embodied carbon to the project.  Mode of transport also impacts emissions, with trucking generally more carbon-intensive than rail and water transport. Heavy materials transported long distances will have a greater carbon footprint than lighter materials due to increased fuel consumption.

  • Example: “Source [insert product here] from manufacturers within a 500 mile radius by trucking, or 2000 mile radius by water.”

Note – realistic expectations and a general knowledge of material source locations should be considered when using this strategy. 

Performance Specifications
An increasingly popular strategy involves rewriting specifications from the typical prescriptive format to a performance-based approach.  Prescriptive specifications give specific direction to material suppliers and installers to ensure a material is manufactured and constructed as they prescribe.  Performance specifications simply specify the desired end result, but do not explain how a product manufacturer should achieve that end result.
Switching to performance specifications changes project workflow by giving more freedom to the material suppliers, rather than having the designers set exact requirements.  In terms of embodied carbon reductions, this freedom for optimization improves the ability of suppliers to reach a lower embodied carbon target than when hindered by unnecessary prescriptive requirements. For example, in concrete specifications the water / cement ratio and prescriptive air content values are examples of these unnecessary prescriptive requirements (in most cases), provided they are replaced with testing and/or modeling to demonstrate the mixture is suitable for the required strength, serviceability, exposure class, and desired service life.
In a performance specification with a goal of reducing embodied carbon, a GWP limit (or carbon budget) is an additional performance characteristic in the specification, and one which should not supersede requirements related to life safety and serviceability. GWP limits should be developed considering the other performance criteria of the structure.
Hybrid specifications involve a combination of prescriptive and performance-based specification language, but prescriptive and performance provisions may conflict, or limit the potential range of solutions available to material suppliers and contractors, and may fail to clearly assign responsibility for the end performance of the materials and structure.
Note – successfully implementing this strategy does require consideration of the range of expertise among potential suppliers.
Resources: 

Global Warming Potential (GWP) Limits
Global warming potential (GWP) limits can be placed on specific materials or project elements.  To date, this has most commonly been applied to concrete mix designs, but in a future with more robust data and EPDs, this could similarly be applied to other products and systems to set maximum limits for GWP.
Determining which GWP baseline values to use is an important step in this process.  The specifier should consider input from the client, contractor, and project delivery team, if possible.  Looking at a baseline average of EPDs in a region is possible with tools such as EC3, which can also provide industry average information to substantiate GWP limits. When making comparisons between EPDs, be sure to confirm that they utilize the same assumptions, life-cycle stages, etc.
GWP limits are most commonly set in performance-based specifications, where they allow the material supplier room to optimize material ingredients to meet a set target.  It is also possible to set GWP limits using prescriptive specifications, but it may be more difficult or costly for the supplier to meet targeted values.  See ‘WBS Strategy 3 – Performance Specifications’ for further information.  See each material section for specific guidance on implementing a GWP strategy for that particular material.

Carbon Bank
A broader strategy for limiting GWP is the ‘Carbon Bank’, or ‘Carbon Budget’ approach.  In this method, an embodied carbon reduction target is set for a portion of the project.  The contractor then chooses a cost-efficient approach to meet the stated target.  For example, a carbon bank could be established for a single sub-contractor such as the concrete supplier. The concrete supplier may then decide to only reduce GWP in the concrete for the building’s foundations, and keep the rest of the concrete as a standard mix, as long as the overall target is met.  This allows more freedom for the contractor to control costs and think creatively to meet the target.  This also creates a creative ‘buy in’ mindset of the contractor and shared ownership in decision making. These interactions facilitate the potential for a positive adoption of sustainability goals.
It is recommended that the specifications ‘bank’ or ‘budget’ is divided between trades to avoid confusion. Setting a carbon ‘bank’ or ‘budget’ for the entire project is likely too confusing for general contractors and leaves significant room for error.
Note – at the time of publishing this guide, setting a Carbon Budget for a new project is largely conceptual due to limitations of project data and benchmarks. A significant goal of the SE 2050 Program and Database is to collect data for setting statistically informed benchmarks and to guide implementation of such strategies.

Sustainability Goals
Specify the project’s sustainability goals in Part 1 – General – Summary. This can be applied to any material specification section, and encourages contractors and manufacturers to work closely with the A/E towards embodied carbon reduction goals.  Thorough communication is encouraged among the project delivery team to make sure goals are met.
Example: This project has a goal of reducing the embodied carbon footprint over a typical project by 20%. To accomplish this goal, we are targeting a carbon footprint reduction for concrete of 35% over the benchmarks established in the concrete industry’s Cradle-to-Gate Life Cycle Assessment Version 3.1.

Structural engineers should be knowledgeable on the topic of carbon offsets, as they may be discussed during conversations with owners and while evaluating product claims in the marketplace.
A carbon offset is a claim of a net reduction in GHG emissions – or an increase in carbon storage (e.g. through the planting of trees) – that is used to compensate for emissions that occur elsewhere, as defined per the Carbon Offset Guide. The rationale behind this strategy is that greenhouse gases mix globally in the atmosphere, thus it does not matter if they are reduced at the source of the emissions or elsewhere.
Rather than a primary carbon reducing strategy, carbon offsets should be considered a supplementary tool for residual project emissions. In other words, carbon offsets should only pay for actions that would not take place without the support of the offsets, which is referred to as “additionality.” Certified Emission Reductions (CERs) and Verified Emissions Reductions (VERs) are two carbon offset certification labels which require consideration of additionality.
Although offsets must be third-party verified, many are controversial; in one example, CERs had been used to support coal-fired electrical generation plants.  Additionality is also difficult to prove in many instances.
Because of these limitations and uncertainties, best practice is to utilize all means of reducing embodied carbon directly, or to make direct reductions through design and material choices, before turning to offsets.
Carbon Offset References:

STRUCTURAL STEEL

General
Approximately 90% of the embodied carbon of fabricated structural steel occurs during the cradle-to-mill-gate Life Cycle Assessment (LCA) stage – module A1. The remainder of the emissions come from l other additive and downstream processes that occur during the production of structural steel, such as bending, galvanization, fabrication, surface preparation and coating, and transportation to job sites – modules A2 through A4. These secondary processes have environmental impacts which are an order of magnitude smaller than those that occur upstream at the steel mill. Therefore, when considering the embodied carbon of structural steel, an engineer should focus on the steel mills that create steel products. The strategies discussed within this section focus on steel sourcing and the implications for embodied carbon.
It’s important to note that unlike other materials, regionality is not as critical a consideration when sourcing steel. Steel products are produced in a discrete number of mills and are distributed all over the country via a network of metals service centers that function as intermediary stock warehouses. The majority of structural steel used in construction is sourced directly from these service centers, not directly from mills. Any embodied carbon reduction specification requirement for fabricated steel will commonly require working with t fabricators and service centers rather than directly with steel mills.

BF-BOF vs EAF
Primary steelmaking, also known as integrated steelmaking, utilizes a Blast Furnace and a Basic Oxygen Furnace (BF-BOF) to produce steel. With this process, virgin iron ore-based inputs are high, recycled content inputs are low, and the primary energy source utilized is derived from coal. Variation in embodied carbon of BF-BOF steelmaking depends on a mill’s input mix of scrap, direct reduced iron (DRI), or pig iron, and the energy grid source mix.
Secondary steelmaking utilizes an Electric Arc Furnace (EAF) to produce steel. With this process, virgin iron ore-based inputs are low, recycled content inputs are high, and the primary energy source utilized is electricity.
On a worldwide average, EAF steelmaking is 75% less carbon intensive than BF-BOF steelmaking, so choosing EAF products can have a large impact on embodied carbon reduction goals.
In the U.S., structural steel products come from both EAF and BF-BOF production, with availability varying by product type – so early coordination with the contractor is critical to confirm the feasibility of procuring EAF steel. Hot-rolled structural steel sections are exclusively EAF, while plate and manufactured products (e.g., HSS, joists, metal deck) may come from either method and require project-specific verification.

Domestic vs Non-Domestic
Overall, the U.S. steel industry is the least carbon-intensive among the world’s leading steel-producing countries. This is due to our high share of EAF steelmaking relative to BF-BOF steelmaking and due to our relatively clean electrical grid. Imported structural products are more likely to be produced in BF-BOFs, as the 2024 worldwide average ratio of BF-BOF:EAF steel production was 71:29, and notably, China’s ratio was 90:10. For comparison, the United States’ ratio was 28:72.
Additionally, not all EAF steel is created equal. In some instances, United States BF-BOF-produced steel may have lower embodied carbon than foreign EAF steel. Material test report (MTR) submittals identify the mill of origin and will confirm whether steel was sourced domestically or non-domestically. AISC maintains a database of shapes and sizes produced domestically for engineers to reference during design. As a practical rule of thumb, sourcing steel produced in the United States is often an effective strategy for achieving lower embodied carbon.

Consider Recycled Content 
There is a correlation between higher recycled content levels and lower embodied carbon intensity in steel, but using one as a proxy for the other may not be fully accurate for a specific product. Mill reporting of recycled content reflects annual averages, not the characteristics of a specific steel product from a specific production heat. In reality, the recycled content of steel products fluctuates from melt to melt, so recycled content letters from mills, which reflect annual averages, may not sufficiently represent the recycled content of an individual product.
Specifying a minimum recycled content percentage is not recommended simply because there are more effective alternatives. However, it is a common sustainability strategy in the marketplace and many green building rating systems utilize this approach for material related credits. Similarly, this strategy may be pursued on projects as an alternative to specifying GWP limits. AISC recommends minimum recycled content values of 75%, 60%, and 50% for hot-rolled sections, steel plate, and hollow structural sections respectively when this specification strategy is implemented.

Lower Embodied Carbon Steel Products
Nearly all of the domestic structural steel producers and manufacturers have published facility-specific EPDs, so it is becoming increasingly viable to directly specify a maximum GWP for these products. (AISC summarizes, links, and accurately interprets all relevant EPDs together at aisc.org/epd and provides specification guidance for maximum GWP approaches in their designer toolkits). A primary decision in this approach is where to set the GWP threshold. A common approach is to set thresholds at industry-average levels, which are based on industry-average EPDs. These EPDs also form the basis of the Carbon Leadership Forum’s material baseline publications. Setting GWP thresholds higher than industry average assures broad compliance while excluding only the highest emitters. Setting GWP thresholds lower than industry average may achieve better embodied carbon performance, but that approach may encounter supply-chain challenges.
Note – Third-party EPD database tools such as EC3 and the Transparency Catalog are other sources of EPD aggregation, but they should not be relied upon for statistical output or for regional benchmarking. In particular, engineers should exercise caution when interpreting EC3’s Boxplot Diagram results for steel. The diagram aggregates many EPDs together that have differing and non-comparable features that affect embodied carbon, and therefore it is not an adequate representation of the steel market at this time. For example, EPDs are lumped together regardless of whether or not they include the effects of fabrication or galvanizing, whether or not the LCA accounting was developed according to a consistent Product Category Rule (PCR), whether or not the LCA modules included are consistent, and whether or not the product fits the category as defined in EC3. Engineers should confirm the EPD assumptions and be specific about parameters when specifying maximum GWP.  

Although the fabrication stage only accounts for approximately 8% of structural steel’s cradle-to-fabricator-gate GWP, fabricators themselves are a key partner on projects pursuing sustainability goals because they are the entity that buys the project’s steel. Fabricators can leverage their supply-chain knowledge to achieve sustainable purchasing for projects and help engineers coordinate practical specification requirements. At the end of 2023, AISC launched a Sustainability Partner Program for their fabricator membership that educates fabricators on their own footprint, commits them to reporting environmental data, and has them create internal sustainability goals. AISC has created the program with the intent to make it easy for fabricators to participate, so it is encouraged to include this requirement in your specification. At a minimum, the program can be a starting point for a sustainability conversation on your steel projects with the fabricator.

Steel Resources:

CAST-IN-PLACE (CIP) CONCRETE

General
Achieving significant embodied carbon reductions in concrete may require deviation from business-as-usual materials, specifications, and project delivery. Structural engineers should engage concrete suppliers, contractors, owners, testing agencies, and other key stakeholders early in design, rather than waiting until construction administration, to understand locally available options and allow adequate time to evaluate and prequalify lower-carbon mixtures.
Strategies may include increased use of blended cements and supplementary cementitious materials (SCMs), performance-based specifications, and alternative cement technologies. Some emerging cement technologies comply with code-accepted standards such as ASTM C595 or ASTM C1157 and should not necessarily be considered experimental. Engineers are encouraged to work closely with local concrete suppliers and innovative technology providers to identify and vet alternatives, including reviewing EPDs to substantiate embodied carbon reduction claims. Arup’s A Framework for Specifying Novel Concrete Technologies provides additional guidance.
As engineers evaluate emerging technologies for potential project use, it is helpful to understand their level of readiness. The Lower Carbon Concrete Guide defines the following categories:

  • Novel: Requires further laboratory testing and validation.
  • Pilot-ready: Supported by laboratory testing but with limited field experience.
  • Market-ready: Tested and commercially available, but may require project-specific evaluation.
  • Project-ready: Tested, approved, and available for the intended project application.

Performance Specifications
Historically, the structural engineering profession has relied on prescriptive specifications to ensure concrete performance, dating back to practices such as specifying minimum cement content and incorporating durability requirements into ACI 318. Minimum cement content was originally prescribed to ensure adequate strength, while prescriptive durability requirements, including maximum water-cementitious materials ratio (w/cm) and air content, served as proxies for long-term durability. Although these requirements have produced durable concrete structures, they prescribe how concrete should be proportioned rather than what performance the concrete must achieve. When considering embodied carbon, exposure class can significantly influence cement content by prescribing by lower w/cm ratios, higher minimum compressive strengths and air content requirements.
Over time, industry research and advancements in concrete materials have improved the understanding of how concrete mixtures achieve strength and durability. As a result, ACI 318 has evolved by introducing durability exposure classes, relaxing w/cm ratios and minimum compressive strength requirements for moderate freeze-thaw exposure, and more recently simplifying the freeze-thaw exposure classifications. Similar refinements have occurred for sulfate, water, and corrosion exposure provisions as the industry has continued moving toward performance-based durability requirements, some of which are offered as alternative compliance paths in the code. Despite these advancements, specifications are often copied from office master specifications or previous projects without considering project-specific exposure conditions, climate, or locally available materials, leaving room for unnecessary conservatism and increased embodied carbon. Structural engineers should carefully evaluate exposure conditions for each project and are encouraged to use the NRMCA Durability Exposure Class resources when selecting durability requirements that appropriately protect the owner’s investment.
As new blended cements, supplementary cementitious materials (SCMs), and admixture technologies continue to enter the market, performance-based specifications are becoming increasingly important. Rather than prescribing mixture proportions, performance specifications establish the required project outcomes while allowing the concrete supplier flexibility to develop the most effective mixture using locally available materials. Developing a successful performance specification requires coordination between the design team, owner, contractor, and concrete supplier to clearly communicate the project’s basis of design, including strength, durability, aesthetics, constructability, schedule, and sustainability objectives. Structural engineers are encouraged to advocate for early coordination between the contractor and concrete supplier during design to identify locally available materials, optimize mixture designs, and fully realize the benefits of a performance-based specification. Refer to the NCSEA Performance-Based Concrete Specifications resource for additional guidance.


Concrete Strength
Over-specifying concrete strength results in increasing the embodied carbon of a given concrete mix. Specify only the strength that is actually required in the design of members and when it is required. If durability provisions in the code require a higher strength, consider taking advantage of that in design. Certain applications may be more challenging to achieve carbon reductions, regardless of specified design strength, for constructability reasons, such as schedule, finishability, and pumpability.
Requiring concrete to achieve its design strength at an early age often increases the embodied carbon because this is typically achieved through higher cement contents. Coordinate strength requirements with the construction team to ensure schedule critical elements achieve strength requirements (e.g. post tensioned members) and explore opportunities to utilize extended long-term strength during design.
If specifying high early strength, also take full advantage of the resulting 28-day or 56-day strength for design. Concrete continues to gain strength well beyond 28 days, especially when including SCMs, when properly cured. Specifying longer moist curing times can allow less over-design of the concrete mix by giving it more time to come up to strength.  Although not a substitute for final acceptance of standard-cured specimens, specifying the use of concrete maturity sensors to monitor early in-place strength can be helpful for advancing construction work, especially when stressing of tendons, removal of formwork, or column installation are on the schedule’s critical path. ASTM C1074 is standard practice for using the maturity method to estimate in-place strength. ACI PRC-228.1-19 is a useful resource with additional background on methods for estimating in-place strength, but cannot be incorporated by reference into specifications and other construction documents.
Reducing the cement content as much as possible will have a significant effect on lowering embodied carbon.  Mixes with less water will meet higher strengths with less cement, however there are practical limits on how much the paste content can be reduced and still meet constructability requirements. Performance specifications for strength and durability can eliminate the need for water/cementitious materials limits, and designers should avoid specifying slump in most instances and let target slump be established by the contractor and concrete producer as needed for constructability. When using performance specifications, allow sufficient time for pre-qualification of mixtures through trial batches, placements, and testing.
Air content also impacts the ability to achieve design strength – in general, higher cementitious materials content will be required for air-entrained concrete. Avoid specifying entrained air except when required for durability purposes to protect against freezing and thawing exposure.
It is also critical that specifications require the testing agency to provide curing on-site and at their laboratory in accordance with initial and standard curing requirements of ASTM C31. Failing to follow standard curing requirements for specimens (normally cylinders) designated for acceptance testing can lead to low strengths, prompting additional overdesign of the mixture to compensate for improper handling of these specimens. Improper initial curing and other testing variability can therefore increase both cement use and embodied carbon. Recent industry guidance and research from NRMCA and the MIT Concrete Sustainability Hub highlight reliable acceptance testing as an important, often overlooked opportunity to reduce concrete embodied carbon.


Supplementary Cementitious Materials and Blended Cements 
Most of the carbon footprint in concrete comes from cement. Reducing cement can be accomplished by using supplementary cementitious materials (SCMs) as a portion of the cementitious materials. SCMs can be separately batched when producing concrete or included when using a blended cement. To allow the most flexibility, permit all types of SCMs in concrete and do not place prescriptive limits on their use, unless required by the code applicable to the project (note that prescriptive SCM limits are only required in ACI 318 for certain circumstances, for example concrete subject to the application of deicing salts).
Some commonly used SCMs used in concrete are fly ash (ASTM 618 Class C and Class F), ground granulated blast furnace slag (slag cement, ASTM C989), or raw or calcined natural pozzolans (ASTM C618 Class N and ASTM C1945), blended SCMs (ASTM C1697), and other pozzolans including ground recycled glass (ASTM C1866). ASTM C1912 is a new performance specification to cover novel SCMs that do not meet other standard specifications and is employed in combination with ASTM C1709’s guide to evaluating alternative SCMs. Regional availability is a factor, checking with local material suppliers to determine what SCMs are available can help engineers plan more achievable low embodied carbon strategies.
Permit the use of blended hydraulic cements (ASTM C595) and hydraulic cement (ASTM C1157) in the specification. The different types of ASTM C595 cements include:

Cement Type Cement Name Limestone Pozzolan Slag Total (Limestone, Pozzolan & Slag)
Type IL Portland-Limestone Cement >5% & ≤15% – – –
Type IP Portland-Pozzolan Cement ≤15% (optional) >0% & ≤40% – –
Type IS Portland Slag Cement
(Note 2)
≤15% (optional) – >0% & ≤95% –
Type IT Ternary Blended Cement ≤15% (optional) ≤40% Note 1 ≤70%
Type IT (S≥70) Ternary Blended Cement
(Note 2)
≤15%
(optional)
Note 1 ≥70% ≤95%
Type IC Composite Cement ≤30% (optional) Note 1 Note 1 ≤70%

Notes:

  1. No stated maximum, but must satisfy limit on total limestone, pozzolan & slag cement.
  2. In practice, Type IS>70 is not permitted for structural applications and has limited availability (applies to both Type IS>70 & Type IT S>70)

ASTM C595 cements with higher SCM contents (30%, or 40% for slag) have lower early-age strength requirements, reflecting the delay in strength development that may be expected.Type IL is generally available in all regions. The same quantity of SCMs can be used in concrete made with Type IL cement as with mixtures with portland cement. Types IP, IS, IT, and IC cements are also growing in availability, although the SCMs in these products vary regionally.
ASTM C1157 (performance hydraulic cements) also include blended cements containing SCMs, but without prescriptive limits on their composition. Blended cements with more ingredients or higher SCM contents than permitted under ASTM C595 can be sold as ASTM C1157 cements.
It may not be feasible to reduce the portland cement content in all concrete mixtures used on a project due to lower strengths, greater setting times, or other factors. Allow suppliers the flexibility to tailor the SCM quantities in concrete mixtures to address sustainability requirements while balancing availability, cost, and performance.
When permitting the use of newer cements and SCMs, communication with the entire project team is critical. A supplier cannot simply substitute one cement type for another in an otherwise unchanged mix without treating it as a new mix design for review and approval.  Different cements have different chemistries and physical characteristics, that in combination with other mixture constituents, can affect setting, workability, and finishing characteristics. Material suppliers are often best positioned to manage the introduction of new cements and SCMs, drawing on their historical data and experience with similar mixtures. Engage suppliers early to determine whether a proposed mixture has an established performance history or requires additional validation. For mixtures developed specifically for the project or otherwise lacking sufficient prior testing, consider specifying pre-qualification testing and mockups. Testing and mockups should be coordinated with the builder, supplier, and design team to confirm that key performance criteria are met for the specific project and application.


Recycled Content 
Recycled water can be permitted by including a reference to ASTM C1602 (instead of specifying potable water). Recycled concrete aggregate (RCA) may also be appropriate for some members, such as footings and foundations. Research has found that up to 25% of natural crushed stone aggregate may be replaced with RCA without significantly affecting concrete strength and recommends partial replacement in moderate exposure conditions (link). However, avoid specifying a minimum recycled aggregate content for concrete as it can have an adverse impact on performance and GWP. ASTM C33, Standard Specification for Concrete Aggregates, now covers recycled aggregates in addition to traditional natural and manufactured aggregates, but notes there are precautions needed with its use, as it may necessitate greater attention to durability and can increase the water demand of mixtures. Refer to Chapter 7 of ACI PRC-221-25 for more information on the use of recycled concrete aggregate. ACI PRC-555-01 also provides guidance on the removal and reuse of hardened concrete.
Note – the embodied carbon benefits of these strategies are hard to quantify since most publicly available concrete carbon calculators do not offer recycled water and recycled aggregate as options.  Moreover, they are not expected to change the GWP of the concrete mix significantly since the GWP factors for water and normal-weight aggregate are small compared to cement but are beneficial when considering resource conservation.


Global Warming Potential Limits:
Global warming potential (GWP) is becoming an increasingly common performance criterion as designers establish embodied carbon limits to meet project sustainability goals and policy requirements. There are several benchmarks and baselines available for establishing GWP limits; however, these datasets should be used carefully, as regional differences in material availability, cement production, and concrete manufacturing practices can create procurement challenges if limits are not tailored to the project location.
Concrete GWP limits may be established on a mix-by-mix basis or using a project-wide carbon budget as demonstrated in ACI 323-24. A project-wide carbon budget is generally encouraged because it provides concrete suppliers flexibility to use higher-GWP mixtures where functionally necessary, such as high-early-strength concrete or post-tensioned slabs, while offsetting them with lower-GWP mixtures where feasible elsewhere on the project. This approach encourages mixture optimization while maintaining the project’s overall embodied carbon target.
Regardless of the approach used, structural engineers are encouraged to advocate for early coordination with the contractor and concrete supplier. Early collaboration allows the project team to understand locally available materials, identify embodied carbon reduction opportunities, optimize mixture designs, and resolve potential procurement challenges before bidding, helping to fully realize the benefits of both performance-based specifications and project-specific GWP limits.
Concrete Baselines:


Lower Embodied Carbon Steel Reinforcement (Rebar)
The embodied carbon of metals depends upon the electricity, fuel sources, and amount of scrap used in production.  In North America, rebar is typically produced from recycled steel in electric arc furnaces (EAFs). EAF steel generally has a higher recycled content and lower carbon footprint than blast oxygen furnace (BOF) steel, although its GWP is highly correlated to the emissions factors associated with the local electrical grid region.
Many rebar producers have published EPDs, so it is becoming increasingly viable to directly specify a maximum GWP for rebar. The EC3 tool can help project teams determine appropriate GWP limits depending on their region and project goals. Because electrical grids can be more or less carbon intensive by region, the industry-wide GWP limits may not be appropriate.


Concrete Resources:

WOOD & MASS TIMBER

General
Wood differs from other structural materials due to its biogenic carbon as a bio-based material. EN 15804+A2, a European standard governing Product Category Rules for Environmental Product Declarations, defines the two different types of carbon as follows:
Fossil carbon: CO2 released from permanent stores, such as fossil fuels.
Biogenic carbon: CO2 stored in bio-based materials such as plants. This carbon is considered part of the Earth’s natural carbon cycle, which is sequestered through photosynthesis and released through either combustion or decomposition.
The SEI Prestandard provides a methodology for calculating biogenic carbon and biogenic carbon flow (when biogenic carbon is sequestered and emitted across a structural system’s lifespan) and when to include in the life cycle assessment. Thorough understanding of these definitions is critical for structural engineers looking to reduce the embodied carbon of their wood and mass timber structures through strategic specifications. Key considerations for procuring climate-friendly wood products are described below, including transportation, adhesives, disclosure, forest management practices, and salvaged wood.

Performance-Based Specifications
Structural engineers have traditionally specified sawn lumber by species and visual grade, which can constrain material sourcing and limit opportunities for optimization. A performance-based specification—defined by required mechanical properties (e.g., strength and stiffness requirements for dimensional lumber and engineered wood products) rather than prescriptive species/grade—enables a broader set of compliant materials, including alternate species. Machine-graded structural lumber, such as machine stress-rated (MSR) or machine-evaluated lumber (MEL), sorts lumber based on mechanical properties that are assigned based on nondestructive bending or tension tests. Because machine grading relies on mechanical tests rather than appearance, machine grading generally leads to more efficient use of timber resources. Not all machine grades are available in all sizes or species, so the specifier must check availability. Engineers are encouraged to include either or both methods in specifications and coordinate with the contractor to choose which method results in the most efficient way to meet the needs of the project.
Performance criteria should be clearly defined within the construction documents, with reference to applicable standards (e.g., American Wood Council NDS provisions and recognized grading rules), and coordinated with the project’s structural analysis assumptions. Engage the design team and owner early to establish acceptance of performance-based substitution pathways prior to contractor selection/procurement, positioning the team to capitalize on material flexibility and supply chain opportunities during bidding and submittal review.
When properly implemented, performance-based specifications allow suppliers to optimize material selection based on regional availability and supply chain constraints, facilitating the use of underutilized species, non-traditional supply streams, and salvaged or reclaimed wood—provided compliance with grading, certification, and durability requirements is demonstrated.
Resources:

Request Environmental Product Declarations
Environmental Product Declarations (EPDs) are available for a wide range of structural wood and mass timber products, including sawn lumber, plywood, oriented strand board (OSB), laminated strand lumber (LSL), laminated veneer lumber (LVL), wood I-joists, glued laminated timber (glulam), and cross-laminated timber (CLT). Structural engineers should incorporate EPD requests into project specifications to support whole-building life cycle assessment (WBLCA), material-level embodied carbon tracking, and to promote robust environmental transparency and traceability from the industry.
When evaluating EPDs, confirm the scope and representativeness of the dataset—specifically whether the declaration reflects an industry-average (regional or national), product-specific, or facility-specific dataset. How biogenic carbon is represented in EPDs can vary internationally. Most North American wood EPDs are cradle-to-gate (Modules A1–A3) and report biogenic carbon content as additional environmental information, along with key parameters such as moisture content, density, and wood fiber composition. EPDs from Europe follow the EN 15804 +A2 which breaks GWP into three categories: GWPfossil, GWPbiogenic, GWPluluc (land use/land use change).
In addition, take note of the declared unit for the wood product. EPDs for dimension lumber or engineered wood products typically declare a standard unit of volume (one cubic meter), but I-joists for example declare a unit of length (one meter).
Industry-average EPDs are commonly available for commodity products such as softwood lumber (often regionally averaged across North America or U.S. subregions). However, industry-average EPDs have not been published in the U.S. for many mass timber products; for example, engineers have used glulam as the proxy material for industry-average CLT modeling data.
Given the current scarcity of facility-specific EPDs for many wood products, structural engineers should coordinate with the design team to request product- or facility-specific EPDs during procurement where feasible.
Resources:

Seek Opportunities for Reclaimed and Salvaged Wood
The reuse of any structural material is often the lowest carbon solution available for structural engineers. The use of reclaimed or salvaged wood has low-carbon benefits not only from lower manufacturing emissions compared to equivalent virgin wood products, but also from the prolonged biogenic carbon storage in the wood element itself.
Even with the implementation of sustainable forest management practices, the logging of virgin timber has environmental impacts. Production emissions include those from logging equipment and transport, partial releases of carbon stored by the soil in below-ground biomass, any manufacturing residues that are incinerated or decomposed in landfills, and the decomposition of logging residues roots, branches, and leaves. For framing lumber, the sum of the upfront manufacturing (A1-A3) emissions is typically greater than the emissions associated with deconstruction, regrading, and reprocessing salvaged lumber. The reuse of existing wood prolongs biogenic carbon storage by giving the material another life in a subsequent structure, extending its total service life.
In order to utilize salvaged wood in a structural application, the design properties (primarily strength and stiffness) of each piece of lumber must be known. Determining design values is easier if the salvaged lumber has an existing grade mark and is free of deterioration. For wood that lacks a grade stamp, identification of the species and structural grading may be required to determine design values. Species identification traditionally involves a wood expert analyzing the specimen under a microscope. Newer methods involve nondestructive evaluation (NDE) techniques such as acoustic grading using wave propagation measurements or DNA analysis of the wood sample. All of these methods, however, are still in development and may require further validation for use with salvaged or reclaimed lumber. Current methods are imperfect and may result in a range of potential species identifications, further complicated by the fact that most commercial groupings include a mix of species.
Grading pieces of salvaged lumber can also be challenging. Regrading a salvaged piece of lumber is not currently allowed by grading agencies because the rules have been developed for newly manufactured lumber.
When a salvaged piece of lumber has an existing grade stamp, the condition must be assessed and deemed free of:

  • Notches or other defects (charring) that reduce net section,
  • Decay or insect damage,
  • Signs of failure or damage from structural loading, deconstruction, or other causes, and
  • Sustained exposure to elevated temperatures over 100 degrees Fahrenheit.

Even when salvaged lumber has an existing grade stamp and passes a condition assessment, a reduction factor applied to the original design values might be warranted to account for uncertainty. The 2027 IBC will include a provision addressing salvaged lumber which prescribes to use not greater than 90% of the design values assigned to the species grade of sawn lumber in the AWC NDS.
For salvage lumber that lacks a grade stamp, a custom program of inspection, grading, and proof testing may have to be developed to substantiate use as a structural component.  Ultimately, the engineer of record bears the responsibility for the species and grading determinations used in structural design.
Quality control measures are critical for successful implementation of this strategy, and the material may require additional testing or treatment before structural reuse is possible.  There may also be jurisdictional requirements prohibiting the use of salvaged or reclaimed wood, and engineers should review the applicable building codes to determine what is allowed for their project.
Tips for using reclaimed & salvaged wood:

  • Prepare performance-based specifications for coordination of reclaimed and salvaged wood with the design team and owner prior to contractor selection and/or procurement. Machine-graded structural lumber requires specification of design stresses (Fb and Ft) and modulus of elasticity (E). Specify machine grades that offer several species options when possible.
  • Investigate opportunities for procuring salvaged wood or wood coming from targeted harvests needed for forest health management by reaching out to local sawmills, foresters, and discussing with suppliers and manufacturers.
  • Search for products through online reuse marketplaces like Heritage Lumber and Cambium Carbon.
  • Engage with reuse communities such as BuildReuse, Unbuilders, Pacific Reclaimed Lumber Supply (Marin County), Building ReSources (San Francisco) The Reuse People (Alameda County) and the Valley of the Sun Reuse/Deconstruction Working Group (VOSWG).

Resources:

Specify Sustainable Forest Management Practices
The net carbon benefit of wood products varies greatly with different forest management practices. Poor forest management practices (e.g., logging on illegal or protected land and clearing of forest for non-forest use) can lead to significant carbon emissions in addition to other negative environmental impacts on ecosystem and forest health. Sustainable forest management practices can vary regionally as different jurisdictions attempt to balance ecosystem health, forest resilience, biodiversity, commercial, and community needs. A well-managed forest can lead to win-win scenarios of maximizing ecosystem health and minimizing emissions into the atmosphere. It is crucial that sustainable forest management is a core criterion for the procurement of sustainable wood products.
According to Think Wood, assurance for timber harvested sustainably can be provided by forest certification, responsible fiber sourcing standards, and/or Best Management Practices (BMPs, developed by every U.S. state). Currently, it is common practice among green building designers to specify certified wood (common programs include FSC, SFI, ATFS, and PEFC) as a means of assuring a baseline of sustainable forest management practices. State-developed Best Management Practices may not be as stringent as the requirements of forest certification, but a few examples of BMPs that are more aligned with forest certification include Oregon’s Forest Production Laws: An illustrated manual, Forest Practices Illustrated: A simplified guide to forest practices rules in Washington State and California’s Forest Practices Act.
While forest product certification that uses a chain-of-custody system is often seen as having a high level of quality assurance for sustainable forest management, direct climate benefits are not necessarily assured by wood certification since these programs are only recently beginning to specifically address climate mitigation. Additionally, certified products may come with a cost premium. Smaller forest owners and public forests can also demonstrate exceptional sustainable forest management practices, but may not have the financial means for acquiring certification. The Climate Smart Wood Group provides guidance on additional criteria for climate-smart forestry operations outside of certification which includes non-industrial timber producers such as “US federal, indigenous or tribal, non-profit organizations and land trusts, and family forest owners.” Other recommendations are sourcing from ecological forestry operations where “restoration is occurring to enhance ecological resilience and integrity (which) by definition offer many climate-smart benefits,” and from forests with above-business-as-usual regulations and practices. Examples of the latter include forests governed by Habitat Conservation Plans and those that are third-party-certified carbon projects.
Given the complexity of wood sourcing impacts and challenges with transparency and traceability, practitioners are encouraged to engage with local foresters who are trained, deeply knowledgeable about local forest needs, and can help identify wood sources from forest management operations. Along with source forest disclosure as described in the next section, it is recommended to request the disclosure of forest management practices.
Various codes and standards seek to establish common practice for sustainable forest management. ISO 38200:2018 sets requirements for the supply chain of wood products. ASTM D7612-21 sets forth minimum criteria and evaluation requirements to categorize wood and wood-based products by their fiber sources, and ASTM D7480-21 is the Standard Guide for Evaluating the Attributes of a Forest Management Plan.,
Recommendations:

  • Request information about forest management practices from manufacturers for wood products.
  • Avoid illegally sourced wood and wood sourced from deforested lands, old growth forests, and protected lands.
  • Proactively engage with forest managers and sawmills, with support from the project team (client, designers, and contractors), to uncover opportunities for available feedstock as byproducts of local forest and ecosystem needs.
  • Evaluate sustainable forest management practices against criteria provided by forestry experts, like the Climate Smart Wood Group procurement guide.
  • Seek indicators of sustainable forest management practices such as forest certification, responsible fiber sourcing standards, Best Management Practices, ecologically-motivated forestry operations, and climate-smart forestry operations from non-industrial timber producers such as the US Forest Service, indigenous or tribal communities, non-profit organizations, and family forest owners.

Request Forest Sourcing Disclosure
The supply chain for wood products tends to be more opaque and harder to trace than for other structural products. Compared to commodity mineral supply chains, the wood supply chain is often more dispersed and has a larger variation in the involvement, attitudes, and intentions of stakeholders (such as local communities, land owners, loggers, mills, manufacturers, developers, the commoditized lumber market, etc.) while also varying from region to region. Engineers can leverage their position as material specifiers by requesting a high degree of traceability and transparency within the forest industry. The World Resources Institute defines these terms as follows:

  • Traceability refers to the ability to link a product with information about its history of locations, owners, and transformations between points in the supply chain.
  • Transparency refers to the making available of information by any stakeholder. This can include broader information that is relevant in the context of halting and reversing forest loss such as sustainability policies and practices, commitments, land use information, monitoring, or outstanding grievances.

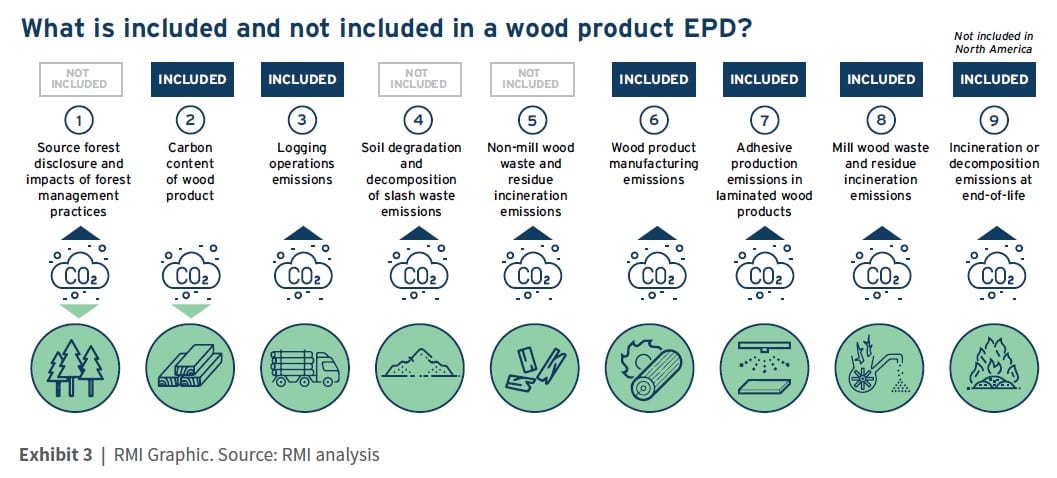
EPDs of structural wood products currently do not include upstream primary data such as source forest disclosure and additional emissions sources. As summarized in the wood chapter of a recent report by RMI, “Greater life-cycle impacts data and transparency of wood products such as EPDs are needed to make better informed choices. Wood products must be sourced and manufactured in ways that go beyond regulatory minimums and foster regenerative and climate-resilient solutions.” As such, it is necessary to request traceability and transparency within the wood supply chain until EPDs are updated to reflect this information.

Source: Driving Action on Embodied Carbon in Buildings (RMI)

Some structural engineers are including questionnaires in their bid documents to collect sourcing information. For example, Davies-Crooks Associates provides one example:
Disclosure Request Template Reference: Timber Forest Sourcing Disclosure Questionnaire (8/21/2023)
Introducing a detailed questionnaire during procurement is a relatively new practice for the industry, and therefore the extent of success and difficulty of this approach are not yet known. It is anticipated that the process will be continually refined for streamlined and practical implementation by users over time. The questionnaire may be included in bid documents to give project teams added transparency about the sourcing of mass timber products. The use of this questionnaire can also provide more accurate transportation data to evaluate the climate impacts of shipping timber products over large distances.
The Climate Smart Wood Procurement Guide, linked in the Wood Resources section, provides more detailed recommendations and guidance on criteria for wood sourcing from a climate-focused perspective.
Recommendations:

  • Aim to use the Timber Forest Sourcing Disclosure Questionnaire (or similar) in your projects.
  • At minimum, request information about the source forest from manufacturers for all wood products above a certain threshold (e.g., > 1% of total construction volume or cost).
  • Examine wood product EPDs for any missing life-cycle impacts data and consider the implications for your project.

Resources:

Transportation Emissions
While manufacturing emissions (A1-A3) for wood products can be low, transportation can substantially add emissions depending on the mode of transportation and distances traveled. Wood product specifiers should therefore pay particular attention to transportation.
Engineers should research the availability and sustainable attributes of wood products in their local region, and specify product requirements that are consistent with the project’s carbon reduction goals. Transportation emissions can vary greatly between different wood products and are a function of the total distance traveled and the mode of transportation utilized. A transportation consideration specific to CLT and some other mass timber products is whether it will be sourced from North America or Europe.
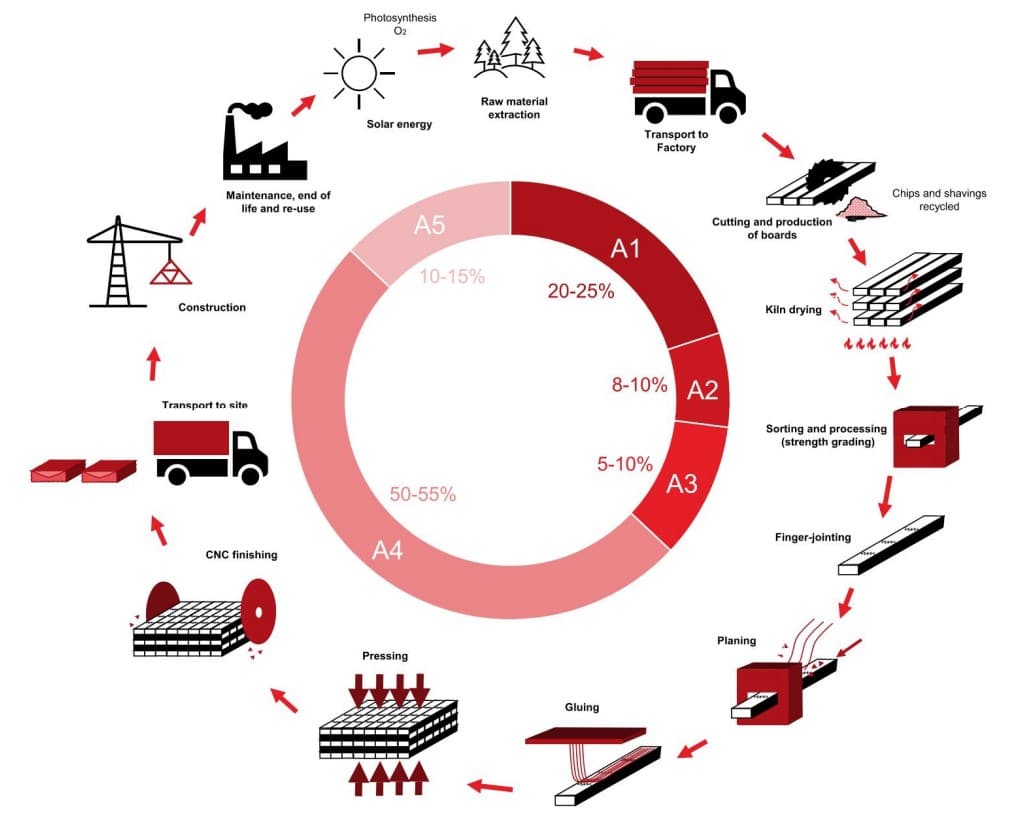
Using WBLCA and EPDs, a UK-based study performed by Arup for CLT and Glulam found that the transportation of the original raw materials to the manufacturing facility (A2) and the transport of manufactured materials to the construction site (A4) respectively accounted for 8-10% and 50-55% of upfront (A1-A5) emissions. It should, however, be noted that the emissions percentages in this study are representative of the UK market, which typically sources from Europe, and the results should not be directly applied to a North American project (where transport distances and modes will vary widely). The results of any WBLCA study are dependent upon multiple factors such as the project location, proximity of mass timber suppliers, and modes of transportation, and the calculation should be performed for each project.

Typical carbon contributions to the supply chain for CLT and Glulam products.

(Note: this study was performed in the UK.)

Source: Embodied Carbon, Timber (Arup)

Recommendations:

    • Weigh the transport emissions (life cycle stage A4) against the manufacturing emissions (A1-A3) to understand the full life cycle emissions associated with use of the wood product. Specifiers should explore these impacts through tools like Forell Elsesser Structural Engineers’ Mass Timber Embodied Carbon tool.
    • Consider locally sourced products to minimize transportation (A4) emissions.
    • Compare the entire upfront carbon emissions (A1- to A5) of products when sourcing materials to be delivered to a specific project site.
    • Consider the entire product lifecycle if possible. Biogenic carbon flows, according to LCA standards, are only considered when the entire product lifecycle is included.
    • Investigate whether lower carbon transport modes are available. Consider prioritizing suppliers that use lower carbon transport modes like rail and cargo ship whenever possible. As the availability of electric vehicles continues to increase, investigate opportunities for electric semi-truck transport.

Acknowledge the Impact of Adhesives
It is important to note that specification of adhesive types is beyond the reasonable scope of the structural engineer, as these are either prescribed by standards, performance requirements, or chosen by the supplier. This section is provided to educate and provide insight into this lesser-known topic.
Many types of wood and mass timber products require the use of adhesive technologies.  While explicit information on the GWP of wood adhesives is limited, some research has shown that adhesives contribute significantly to the GWP of wood-based products.
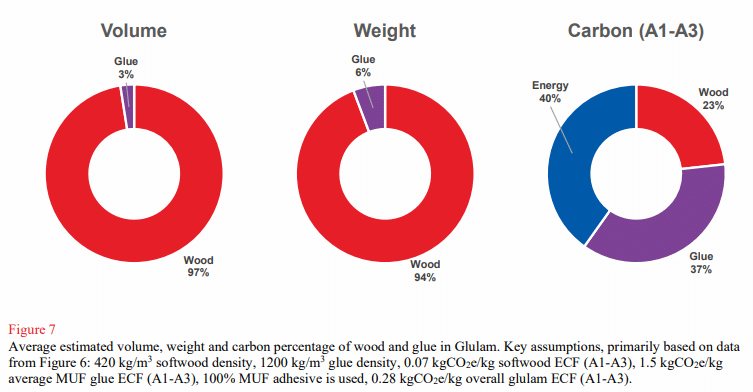
Adhesives are typically made from oil, which is energy-intensive to extract and refine. CLT and Glulam products typically contain at least 1 to 2.5% by volume of adhesive, yet the specific percentage of a product’s GWP that is due to adhesives is not consistently reported in EPDs.  Researchers at Arup have put together the graphic below from a variety of resources to provide a comparison of volume, weight and carbon for glulam timber.

Source: Embodied Carbon, Timber (Arup)

Acknowledge the Impact of Kiln Drying
It is important to note that specification of kiln drying methods is often beyond the reasonable scope of the structural engineer, as these are either prescribed by standards or chosen by the supplier.  This section is instead provided to educate and provide insight into this lesser-known topic.
Wood is a hygroscopic material that absorbs and releases moisture into the surrounding atmosphere. Wood has improved strength and stiffness when dry compared to wet, and wood shrinks as it undergoes the drying process – causing surface cracks (checks). To ensure dimensional stability, avoid visual cracks, and benefit from the improved mechanical properties, wood is typically dried to approximately 12% moisture content – the typical equilibrium moisture content of a building. Wood for laminations (lamstock) in CLT and glulam is typically dried to a moisture content of less than 16% to ensure proper adhesion of the laminations.
Wood can be dried by air flow (wood stickered and stacked outside), in a solar kiln (wood stickered and stacked within a greenhouse), or dried in a fueled convective kiln. (Stickers are wood spacers placed between the boards to allow the air to circulate.) Air drying uses no additional energy but may take months to reach the desired moisture content. Solar kilns use a small amount of electricity to power fans to circulate air, but may take 4-6 weeks to reach the desired moisture content. Convective kilns require energy input to heat the air, but can dry wood in days. Convective kiln drying is the typical method for commercial wood and laminated wood products.
The kiln drying process consumes around 90% of the manufacturing energy of sawn wood products. The fuel used for the kiln depends on the facility location and operator, but typically will be a mix of incinerated biomass from the facility’s process and natural gas. Some studies have indicated that between 35% and 40% of the Global Warming Potential of glulam can be attributed to lamstock production, which is associated with this drying process.
While it is often impractical to specify the drying method, this should be visible in the product EPD. Facilities that use a larger proportion of non-fossil fuels for their kiln or have a local renewable energy grid will have a lower carbon footprint. For unlaminated wood products in some environmental conditions, the emissions associated with drying can also be avoided by specifying green (undried) lumber with a moisture content of 20% or above and allowing the material to dry naturally.

<strong”>Additional Considerations for Structural Engineers
SHEATHING | The 2020 AWC/CWC industry-average Environmental Product Declarations (EPD) indicates that OSB has over 10% more cradle-to-gate embodied carbon (A1 – A3) than softwood plywood. OSB, however, has a higher fiber density and therefore biogenic carbon content that is 15%-38% greater than softwood plywood. Structural products made from strands, furthermore, utilize more of the log than veneer products that generate more residues that must find other uses to avoid waste. OSB and plywood are generally equivalent as structural sheathing materials, though OSB typically has a slightly higher apparent shear stiffness while plywood has a higher bending stiffness.The latest OSB and plywood EPDs can be found through a search of the American Wood Council resources.
OTHER WOOD USES | The construction industry often requires the use of wood-based products for ultimately non-structural applications, most notably including concrete formwork and temporary structures such as shoring. Structural engineers should consider these other uses of wood when revising procurement documents for sustainability, and apply the strategies listed in this resource where applicable (formwork is often specified in the Division 03 concrete specifications, for example).

CONCRETE MASONRY UNITS (CMU)


CMU assemblies are a composite system of four materials, each of which can be addressed in specifications: concrete block, mortar, grout and steel reinforcement. Concrete masonry walls provide structure while also forming a major component of the building enclosure.

Specified Masonry Compressive Strength (f’m)
The compressive strength of masonry used in design is a composite measure of the type of mortar (Type M, S, or N) used in construction, the compressive strength of the CMU, and the compressive strength of the grout, if used. TMS 402/602 includes two options for verifying f’m:

  1. Unit Strength Method – a codified correlation between the compressive strength of the CMU and the type of mortar used in construction. When using the unit strength method, the specified compressive strength of the grout (f’g) must equal or exceed the specified masonry compressive strength (f’m).
  2. Prism Test Method – using units, mortar, and grout (if used) from the project, prism samples are constructed, cured, and tested. The resulting measured compressive strength must equal or exceed f’m.

Because the unit strength method is a statistical correlation to individual material strengths, there is a degree of conservatism built into this approach. At the lower range of assembly compressive strengths (e.g., f’m = 2,000 psi) the selected testing method may not change the selected products or embodied carbon of the end result, so it is usually not economical to do the additional testing required by the prism test method. This is primarily because a lower-strength block (unit strength<2,000 psi) is not available. At the upper range of assembly compressive strengths (e.g., f’m = 3,000 psi), testing is generally beneficial and could lead to material and embodied carbon savings.
Engineers are encouraged to include either or both methods in specifications and coordinate with the contractor to choose which method results in the most efficient way to meet the needs of the project

Supplementary Cementitious Materials
Using supplementary cementitious materials (SCMs) to replace a portion of the portland cement in the concrete block and/or grout can reduce concrete masonry’s carbon footprint. Both ASTM C90, Standard Specification for Dry-Cast Loadbearing Concrete Masonry Units, and ASTM C476, Standard Specification for Grout for Masonry, permit several options for including SCMs.
Some commonly used SCMs in the manufacture of concrete masonry block and grout are fly ash, ground granulated blast furnace slag (slag cement), raw or calcined natural pozzolans, and other pozzolans including ground recycled glass. Ground glass pozzolans conforming to ASTM C1866 may be used in grout. Blended cements may also be utilized, including Type IP (with pozzolans), Type IS (with slag) and Type IL (portland-limestone cement). Type IL is becoming more and more prevalent for both blocks and grout. If architecturally finished CMU are used on a project, SCM use may affect color. Regional availability is also a factor, so checking with local producers to determine what SCMs are available can help engineers plan for low embodied carbon strategies.

Natural Versus Lightweight Aggregates
Lightweight aggregate used to produce lower density CMU can be manufactured (such as expanded shale), naturally occurring (such as pumice or scoria), or derived from by-products of other industrial processes (such as slag or bottom ash). Manufactured lightweight aggregate has higher embodied carbon compared to naturally occurring lightweight aggregate because of the energy required to produce it. It is important to note that the type of lightweight aggregate available to CMU manufacturers varies by geographical region. As such, they should be consulted to determine what type of lightweight aggregates are regionally available when weighing the option of specifying lightweight block. Specifiers should also review EPDs for aggregate type when available. The industry average EPD provides separate categories for not only strength ranges, but also lightweight aggregate type, reporting natural lightweight aggregate and manufactured lightweight aggregate as separate categories.
Performance characteristics dependent on density should be considered when specifying the density of CMU, such as fire ratings, R-values, and STC ratings. Mason contractors may prefer lightweight units to increase their productivity. Unit compressive strength is independent of unit density as all units must meet minimum specified strengths regardless.

Carbon Reduction Technologies
Because of the way CMU are manufactured, there are several manufacturing innovations that can reduce the embodied carbon associated with CMU construction. Strategies include technologies that encourage more CO2 sequestration via concrete carbonation, such as using aggregates that are pre-carbonated, injecting CO2 directly into the mixture or utilizing specialized curing systems. Alternative cements are also being developed that lower embodied carbon by changing the way they are made.

Mortar
Mortar used in masonry construction falls into one of three categories based on cement type: portland cement/lime mortar, mortar cement mortar, and masonry cement mortar. Mortar cement and masonry cement mortars have much lower global warming potential compared to conventional portland cement/lime mortar because these cements already typically contain a high proportion of filler material such as limestone powder. Masonry cement mortars can be used in most regions, except in areas where Portland-lime mortar is required for high seismic structural masonry. Availability of mortar EPDs in the United States to quantify differences in emissions is limited at this time. To help estimate the embodied carbon of mortar, ASTM C270 proportion specification requirements can be followed. Depending on the mortar type, cements generally make up about 15% of the volume in a mortar mix.

Grout
It is recommended to specify the compressive stress method instead of the volume method to proportion grout mix. ASTM C476, Standard Specification for Grout in Masonry, permits the grout to be proportioned by volume (prescriptive) or using specified compressive strength in accordance with ASTM C1019 (performance). Using the compressive strength method generally results in less cement, thereby reducing embodied carbon.
Grout can be specified as either fine grout or coarse grout. Fine grout, with aggregate sizes typically less than 1/8 in., are appropriate when grouting highly congested masonry assemblies. The trade-off when using fine grout is that there is typically an increased demand for more cement in the mix due to the larger surface area of smaller aggregates compared to larger aggregate gradations.
Self-consolidating grout is also an option with masonry construction, however, to maintain a stable, flowable mix using self-consolidating grout, a very high cement content is required, often resulting in grout compressive strength in excess of 7,000 psi and an increase in embodied carbon.

Lower Embodied Carbon Steel Reinforcement (Rebar)
The embodied carbon of metals depends upon the electricity source used in production. Rebar In North America is typically produced in electric arc furnaces (EAFs). EAF steel generally has a higher recycled content and lower carbon footprint than blast oxygen furnace (BOF) steel, see the steel specification guidance section for additional information.
Many rebar producers have published EPDs, so it is becoming increasingly viable to directly specify a maximum GWP for rebar. See the whole building strategy – promote transparency and disclosure section for more information on EPDs.
Joint reinforcement is less likely to be produced in an EAF and specifiers are urged to investigate the availability of lower-carbon products.

Resources:

ACKNOWLEDGEMENTS

Thank you to the following for your contributions to this document.

  • Charlotte Ochoa
  • Mark Webster, SGH
  • Chelsea Drenick, WoodWorks
  • Michael Cropper, Thornton Tomasetti
  • David Shook, Skidmore, Owings & Merrill
  • Carl Elefante, Architecture 2030
  • Lindsay Rasmussen, RMI
  • Brian Trimble, International Masonry Institute 
  • Jonathan Tavarez, American Institute of Steel Construction
  • Max Puchtel, American Institute of Steel Construction
  • Scott Campbell, National Ready Mixed Concrete Association
  • Truc (Tracy) Huynh, RMI
  • Dan Bergsagel, sbp
  • Jessica Martinez
  • Eric Giannini, American Cement Association
  • Heidi Jandris, Concrete Masonry and Hardscapes Association
  • Marco Lo Ricco, U.S. Department of Agriculture
  • Eli Rose, WSP
  • Olivia Paxson, KPFF
Back to top of page